New
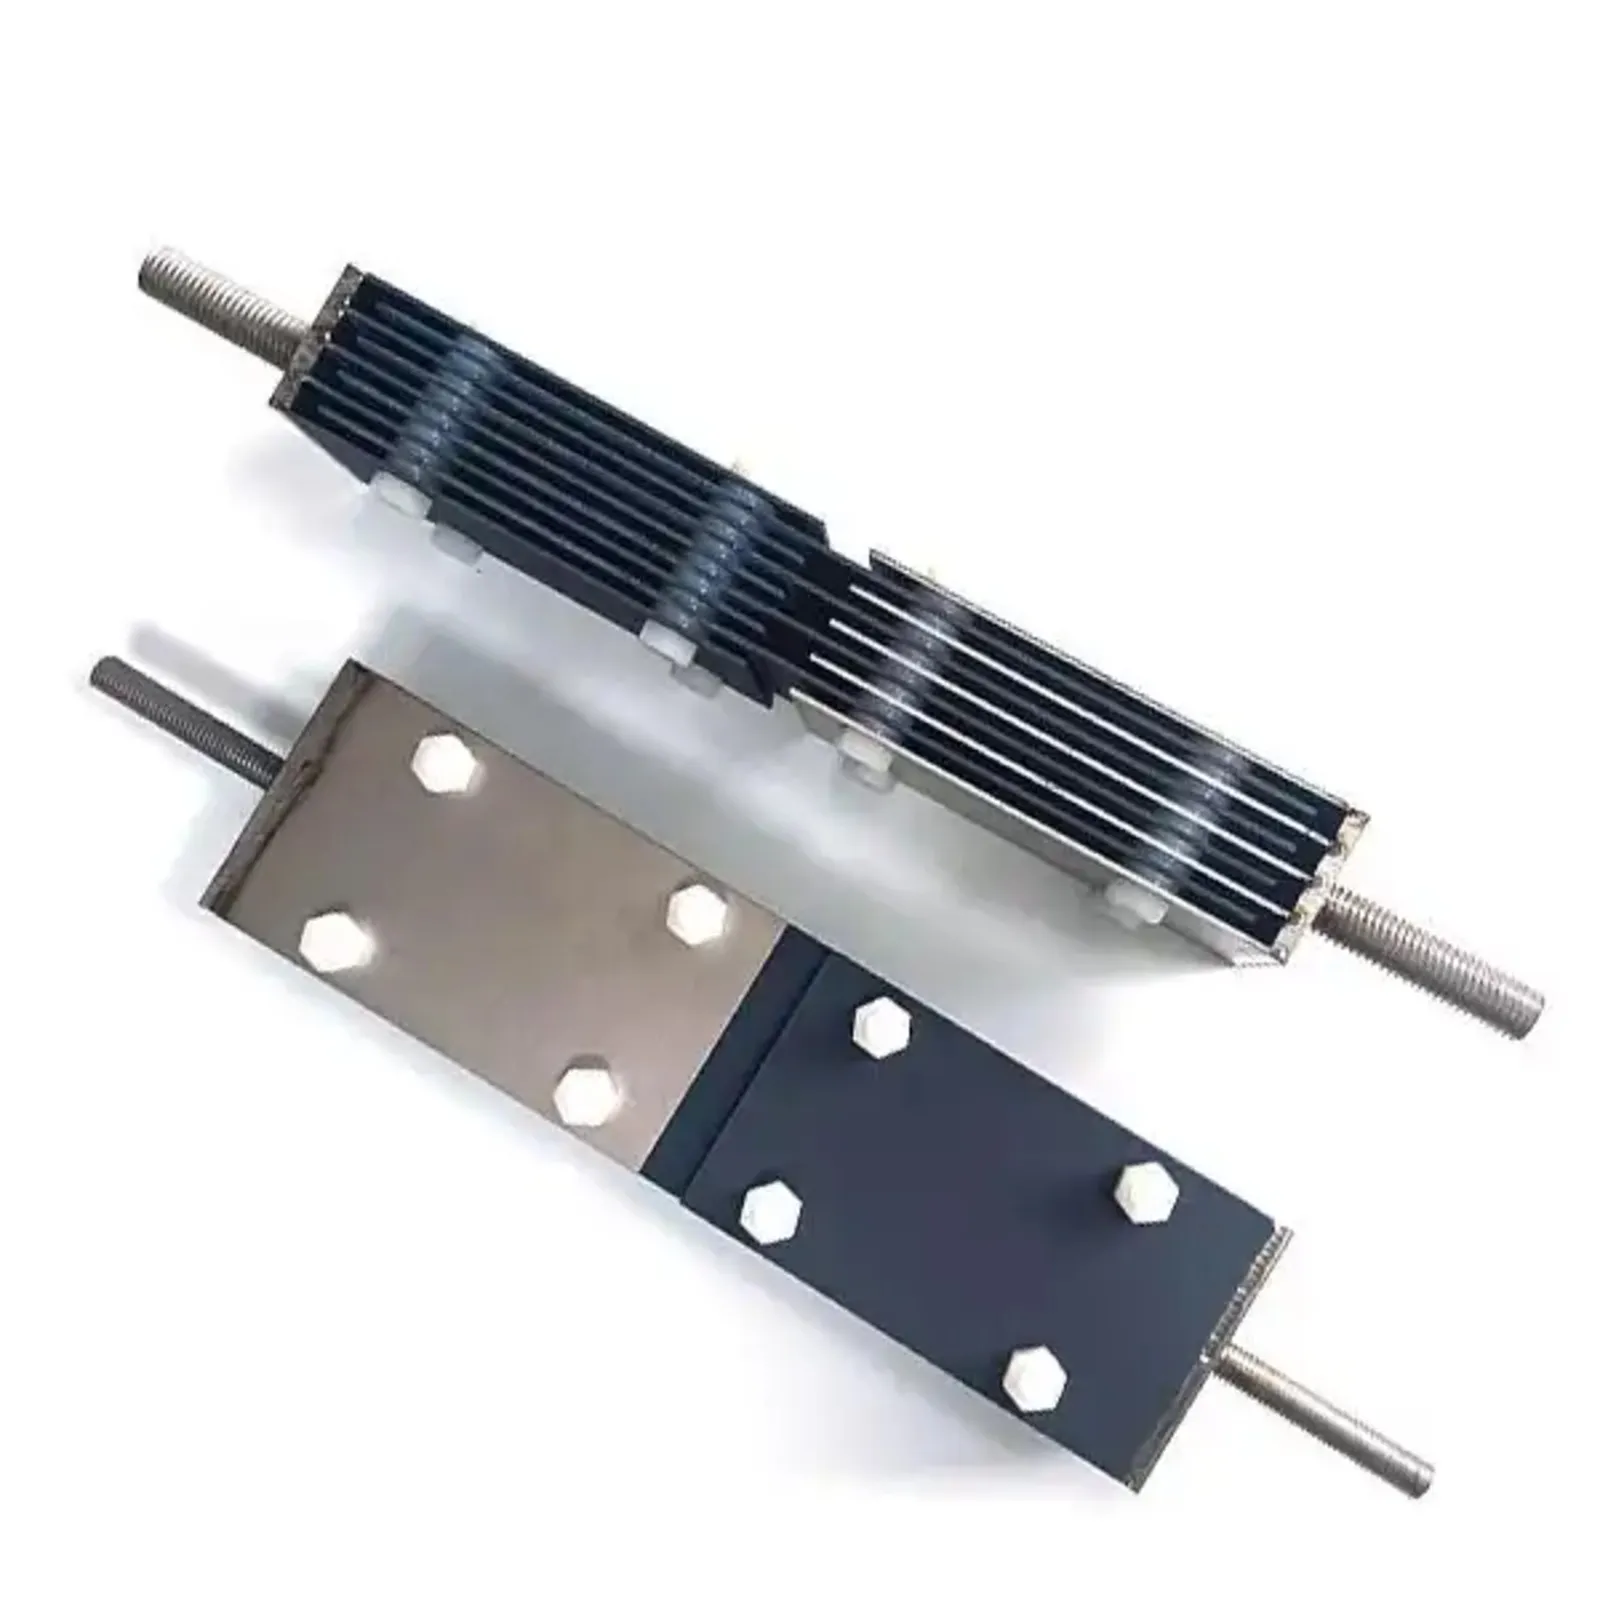
Titanium Anode for Sodium Hypochlorite Generator
Price
$20.00
- $2,000.00
/ PC
MOQ: 1 PC
Product Description
Frequently Asked Questions
What is a titanium anode in a sodium hypochlorite generator?
A titanium anode is the working electrode at the heart of a sodium hypochlorite generator. It oxidizes chloride ions in saltwater into chlorine gas, which reacts in the electrolyte to form sodium hypochlorite (NaOCl), the active disinfectant. The anode consists of a commercially pure titanium substrate (Grade 1 or 2) coated with a mixed metal oxide (MMO/DSA) layer of ruthenium, iridium, and titanium oxides. Titanium gives the electrode corrosion resistance and dimensional stability; the MMO coating keeps chlorine overpotential low, which reduces power consumption. Under normal brine conditions, a properly rated MMO anode delivers 3–5 years of service and can be recoated at end of life.
What is the difference between an MMO anode and a DSA anode?
They refer to the same thing in practice.MMO(mixed metal oxide) describes the catalyst coating—thermally decomposed ruthenium, iridium, tantalum or titanium oxides.DSA(dimensionally stable anode) is the industry name popularized for the same electrodes, emphasizing that the anode does not change shape during electrolysis. In procurement you will see both terms used interchangeably for Ru-Ir and Ir-Ta coated titanium electrodes.
How does an onsite sodium hypochlorite generator work?
A dilute brine (about 3% NaCl) or seawater is passed through an electrolytic cell. At the anode, chloride is oxidized to chlorine gas (2Cl⁻ → Cl₂); at the cathode, water is reduced to hydrogen and hydroxide. The chlorine and hydroxide immediately react in solution to form sodium hypochlorite (NaOCl), a safe liquid disinfectant dosed directly into the water stream. The titanium anode’s coating determines how efficiently this chlorine-evolution reaction proceeds.
What is MMO coating loading and why does it matter?
Coating loading is the mass of noble-metal oxide catalyst applied per square meter of anode surface, typically8–15 g/m²for hypochlorite anodes. Higher loading generally means longer service life because more active catalyst is available as the surface slowly deactivates. Loading below 6 g/m² shortens life sharply; loading above 20 g/m² gives diminishing returns and can crack. We adjust loading to your target current density and warranty period.
Are ruthenium and iridium precious metals?
Yes—ruthenium and iridium are platinum-group metals and their prices do fluctuate on global markets, which affects anode cost. Ru-Ir coatings are usually more economical because ruthenium is cheaper than iridium. Ir-Ta coatings cost more but last longer in seawater. We quote against current metal prices and can lock pricing for scheduled orders; re-coating spent anodes also hedges against metal-price exposure because the substrate is reused.
Why does chlorine evolution efficiency matter?
Chlorine evolution efficiency determines how much of the applied electrical current is converted to active chlorine versus wasted on side reactions (oxygen evolution, heat). Higher efficiency means lower energy cost per kg of NaOCl produced, smaller power supply requirements, and less waste heat to manage.
How do I size an anode to my electrolyzer output?
Start from your target chlorine output (g/h or kg/h) and Faraday’s law: roughly1 g of chlorine per ampere-hour. Divide the required current by your chosen current density (A/m²) to get the active coating area. Add margin for efficiency (use 85–90%). Provide this area, your electrolyzer internal dimensions, the brine concentration and the connection method, and we engineer the mesh/plate layout and coating.
Can titanium anodes be customized to my electrolyzer?
Yes. As a factory we produce OEM anodes to your drawings: expanded mesh, perforated plate, sheet, rod, tube, ribbon or complex welded assemblies. Provide your electrolyzer dimensions, coating area, current density and connection method (titanium bolt, lug or welded titanium bar), and we deliver samples within7–10 working days for approval before mass production.
What shapes and connections are available?
Common shapes are expanded titanium mesh (most economical, good flow), perforated or solid plate, rod, tube and ribbon. Connections are made by titanium bolts, threaded lugs, or a welded titanium conductor bar that links multiple mesh panels into one assembly. The connection point is left uncoated to allow welding and is passivated to resist corrosion.
How do I clean and maintain the anode?
In hard-water areas, calcium and magnesium scale deposits build up on the anode and reduce efficiency. Clean with a weak acid wash (5–10% hydrochloric or citric acid) for 10–30 minutes, then rinse with fresh water. Never scrape the coating with metal tools or use strong mineral acids at high temperature, as this damages the MMO layer. Soft-feed brine and periodic acid washing extend coating life.
Does polarity reversal harm the anode?
Brief, controlled polarity reversal is sometimes used to descale cathodes automatically, but frequent or prolonged reversal drives oxygen-evolution and anodic dissolution that wears the MMO coating faster. If your system uses polarity reversal, tell us so we can select an Ru-Ir formulation and loading optimized for reversal duty, and limit reversal duration per the cell manufacturer’s guidance.
What is a titanium anode in a sodium hypochlorite generator?
A titanium anode is the working electrode at the heart of a sodium hypochlorite generator. It oxidizes chloride ions in saltwater into chlorine gas, which reacts in the electrolyte to form sodium hypochlorite (NaOCl), the active disinfectant. The anode consists of a commercially pure titanium substrate (Grade 1 or 2) coated with a mixed metal oxide (MMO/DSA) layer of ruthenium, iridium, and titanium oxides. Titanium gives the electrode corrosion resistance and dimensional stability; the MMO coating keeps chlorine overpotential low, which reduces power consumption. Under normal brine conditions, a properly rated MMO anode delivers 3–5 years of service and can be recoated at end of life.
What is the difference between an MMO anode and a DSA anode?
They refer to the same thing in practice.MMO(mixed metal oxide) describes the catalyst coating—thermally decomposed ruthenium, iridium, tantalum or titanium oxides.DSA(dimensionally stable anode) is the industry name popularized for the same electrodes, emphasizing that the anode does not change shape during electrolysis. In procurement you will see both terms used interchangeably for Ru-Ir and Ir-Ta coated titanium electrodes.
How does an onsite sodium hypochlorite generator work?
A dilute brine (about 3% NaCl) or seawater is passed through an electrolytic cell. At the anode, chloride is oxidized to chlorine gas (2Cl⁻ → Cl₂); at the cathode, water is reduced to hydrogen and hydroxide. The chlorine and hydroxide immediately react in solution to form sodium hypochlorite (NaOCl), a safe liquid disinfectant dosed directly into the water stream. The titanium anode’s coating determines how efficiently this chlorine-evolution reaction proceeds.
What is MMO coating loading and why does it matter?
Coating loading is the mass of noble-metal oxide catalyst applied per square meter of anode surface, typically8–15 g/m²for hypochlorite anodes. Higher loading generally means longer service life because more active catalyst is available as the surface slowly deactivates. Loading below 6 g/m² shortens life sharply; loading above 20 g/m² gives diminishing returns and can crack. We adjust loading to your target current density and warranty period.
Are ruthenium and iridium precious metals?
Yes—ruthenium and iridium are platinum-group metals and their prices do fluctuate on global markets, which affects anode cost. Ru-Ir coatings are usually more economical because ruthenium is cheaper than iridium. Ir-Ta coatings cost more but last longer in seawater. We quote against current metal prices and can lock pricing for scheduled orders; re-coating spent anodes also hedges against metal-price exposure because the substrate is reused.
Why does chlorine evolution efficiency matter?
Chlorine evolution efficiency determines how much of the applied electrical current is converted to active chlorine versus wasted on side reactions (oxygen evolution, heat). Higher efficiency means lower energy cost per kg of NaOCl produced, smaller power supply requirements, and less waste heat to manage.
How do I size an anode to my electrolyzer output?
Start from your target chlorine output (g/h or kg/h) and Faraday’s law: roughly1 g of chlorine per ampere-hour. Divide the required current by your chosen current density (A/m²) to get the active coating area. Add margin for efficiency (use 85–90%). Provide this area, your electrolyzer internal dimensions, the brine concentration and the connection method, and we engineer the mesh/plate layout and coating.
Can titanium anodes be customized to my electrolyzer?
Yes. As a factory we produce OEM anodes to your drawings: expanded mesh, perforated plate, sheet, rod, tube, ribbon or complex welded assemblies. Provide your electrolyzer dimensions, coating area, current density and connection method (titanium bolt, lug or welded titanium bar), and we deliver samples within7–10 working days for approval before mass production.
What shapes and connections are available?
Common shapes are expanded titanium mesh (most economical, good flow), perforated or solid plate, rod, tube and ribbon. Connections are made by titanium bolts, threaded lugs, or a welded titanium conductor bar that links multiple mesh panels into one assembly. The connection point is left uncoated to allow welding and is passivated to resist corrosion.
How do I clean and maintain the anode?
In hard-water areas, calcium and magnesium scale deposits build up on the anode and reduce efficiency. Clean with a weak acid wash (5–10% hydrochloric or citric acid) for 10–30 minutes, then rinse with fresh water. Never scrape the coating with metal tools or use strong mineral acids at high temperature, as this damages the MMO layer. Soft-feed brine and periodic acid washing extend coating life.
Does polarity reversal harm the anode?
Brief, controlled polarity reversal is sometimes used to descale cathodes automatically, but frequent or prolonged reversal drives oxygen-evolution and anodic dissolution that wears the MMO coating faster. If your system uses polarity reversal, tell us so we can select an Ru-Ir formulation and loading optimized for reversal duty, and limit reversal duration per the cell manufacturer’s guidance.
Trade Information
Delivery Time
15-25
Days
Supply Ability
2,000 Pieces/month